static
Amihan STOL design specifications
 Amihan STOL — Design Specification Book
A living document. Every design decision recorded with its reasoning. Add to it as the design evolves — nothing here is locked unless explicitly stated.
CHAPTER 1 — PROJECT GOALS & DESIGN PHILOSOPHY
What This Aircraft Is For
The Amihan STOL is a two-seat, high-wing, cantilever monoplane designed for short-field and water operations in a coastal and island environment. It is designed to operate from short gravel strips, beaches, and sheltered water — the kind of terrain where a standard light aircraft is marginal and a floatplane is the normal answer. The goal is an aircraft that is genuinely capable in that environment, not merely certificated for it.
Primary roles:
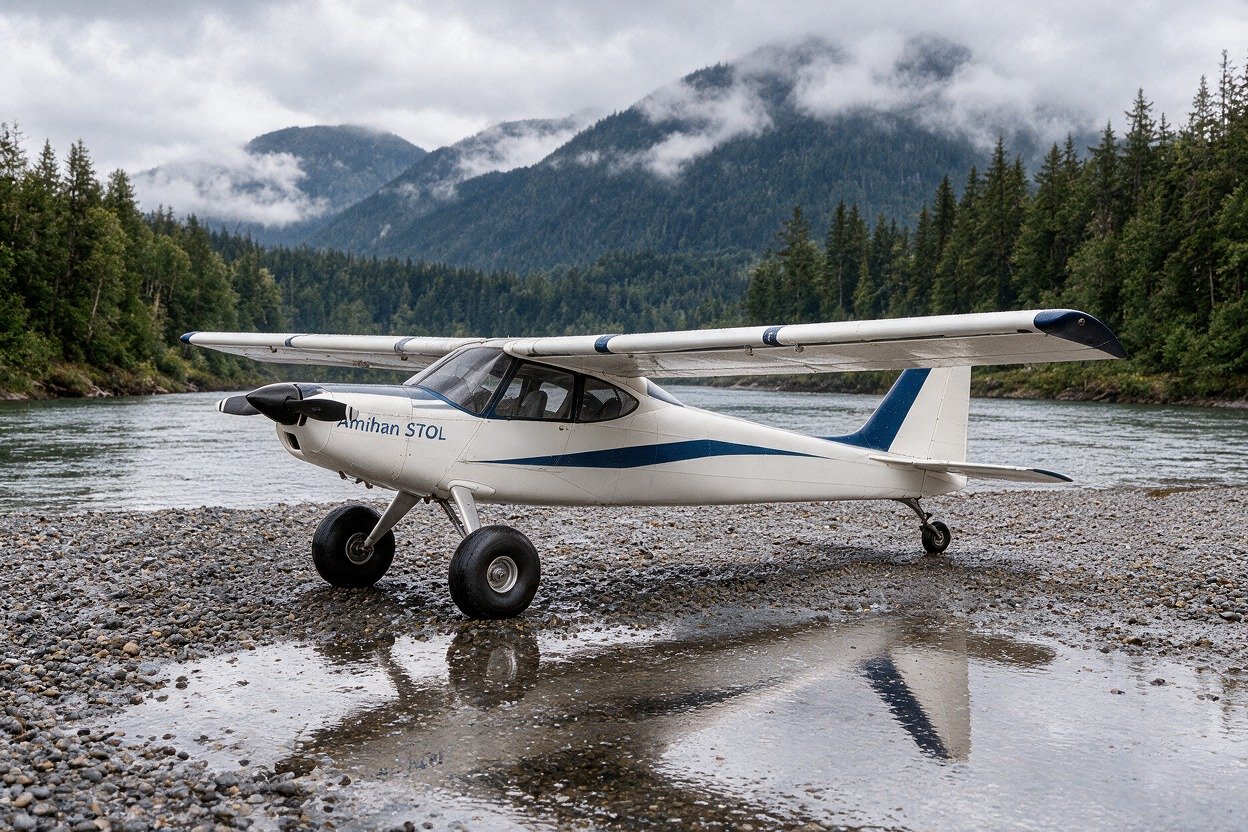
- Short-field bush flying — wheels on gravel, grass, or packed sand
- Float operations — calm and moderate sea state
- Cross-country cruise at 150 knots — the aircraft should not be slow everywhere, only slow when it needs to be
- Emergency and utility use — the kind of aircraft that earns its keep
The Helio Courier as Inspiration
The Helio Courier is the reference aircraft for this design. It achieves a stall speed of approximately 30 mph at 2,800 lb gross through a combination of fixed full-span leading-edge slats, large Fowler flaps, full-span drooping ailerons (flaperons), and a clean high-aspect-ratio cantilever wing. It does this without tricks — the aerodynamics are honest and the slow-flight handling is docile.
The Amihan takes the same approach: invest the complexity budget in the high-lift system, keep the rest of the aircraft straightforward, and let the wing do the work.
The Modular Platform Concept
The Amihan wing is designed to serve two aircraft:
- Amihan Glider — 42 ft span, foot-launched, single seat, ~385 lb gross. The original design. A soaring aircraft built for efficiency and foot-launchability.
- Amihan STOL — same planform, same chord, same rib tooling and skin moulds, powered by the UL Power 520iS, side-by-side two seats, float or wheel undercarriage.
The two aircraft use different spars (different structural ratings) but share identical root pin geometry, root rib layout, and leading-edge tang position. The carry-through beam and fuselage-side hardware never change. Swapping between configurations is a matter of pulling three pins and lifting the wing clear.
This is not a compromise — it is a deliberate engineering constraint that forces the two designs to stay compatible at every interface that matters.
Design-To / Operate-At Weight Strategy
The Amihan STOL is designed to the 2,000 lb structural case (utility category, +3.8G/-1.5G limit, +5.7G/-2.25G ultimate) while targeting approximately 1,200 lb operating gross weight. The actual loaded weight with two crew, full fuel, and baggage comes out to approximately 1,440 lb — well within the structural envelope and comfortably below the 2,000 lb design case.
The purpose of this margin is not conservatism for its own sake. It is room to grow — heavier floats, additional equipment, a heavier engine variant — without triggering a structural redesign. The spar is sized once, correctly, to the 2,000 lb case. Everything else is sized to the real operating weight.
Design Philosophy in Summary
- Build to real numbers, not optimistic ones
- Invest complexity where it buys performance — the high-lift system — not where it merely adds features
- Keep every load path explicit and inspectable
- Design for the marine/float environment from the start, not as an afterthought
- The experiment decides, not the theory — build, measure, adjust
CHAPTER 2 — AIRFRAME GEOMETRY
Overall Dimensions
ParameterValueNotesWing span42 ft (12.8 m)Full span, tip to tipWing chord4 ft (1.22 m), constantNo taper — simplifies tooling, ribs, skin mouldsWing area168 sq ft (15.6 m²)Span × chordAspect ratio10.5Span² / area — high for a powered aircraft; good for cruise efficiency and glideWing sectionNACA 65(2)-415Laminar-flow section, 15% thickness, max thickness at ~35% chordFuselage length22 ft (6.7 m)See tail moment arm rationale, Chapter 5Cabin width43 in (1.09 m)Matches PA-28-140 / Cessna 172 — proven side-by-side widthWing positionHigh wing, cantileverCarry-through above cabin roofSeat arrangementSide-by-side, two seatsPilot and passenger abreastUndercarriageWheels standard; floats possibleFloat attach geometry to be designed in from the start
Fuselage Length Rationale
An initial 20 ft fuselage was considered. At 20 ft, the wing-AC-to-stabilator moment arm is approximately 10 ft, which forces a ~27 sq ft stabilator and leaves the full-flap pitch trim margin uncomfortably tight — the additional downwash from full flaps risks consuming most of the stabilator's available nose-up authority at the point it is needed most (the flare).
At 22 ft, the moment arm grows to approximately 12 ft. The required stabilator area drops to ~22 sq ft, the trim range stays at the original ±5°, and the full-flap downwash margin becomes comfortable. The weight penalty for the extra 2 ft of aft fuselage is approximately 5-15 lb, partly offset by the lighter stabilator. The fuselage-to-span ratio at 22 ft is 0.52, comparable to the Helio Courier (0.54) and Cessna 185 (0.56).
Cabin Width Rationale
43 in matches the PA-28-140 (Cherokee 140) and Cessna 172 — proven, well-understood cabin widths for side-by-side seating. The carry-through beam spans 43 in at the cabin roof, keeping it short and light. Reference widths for context: Cessna 182/185 = 44 in, Helio Courier = 46 in, Piper PA-32 = 49 in, Sling High Wing = 47.2 in.
Wing Position and Carry-Through
High-wing configuration with the carry-through beam above the cabin roof. The main spar sits at 35% chord (the NACA 65(2)-415's maximum thickness location), which corresponds with the rear door post. This ties the primary wing structure directly to a major fuselage frame.
The carry-through is a short aluminium box beam spanning the 43 in cabin width at roof level, with steel lug ears at each end. Both the glider spar and the STOL spar attach to the same carry-through via identical pin geometry — no fuselage modification required to swap wings.
CHAPTER 3 — WING DESIGN
Aerofoil Section
The wing uses the NACA 65(2)-415 throughout the full span. This is a laminar-flow section with maximum thickness at approximately 35% chord — further aft than a conventional 4-series section. It delivers low cruise drag when the boundary layer stays attached, and reasonable lift characteristics at low speed when assisted by the slat system. The slat carries the high-lift burden entirely; the main element does not need to be a high-camber section.
When the slats deploy, the main element's exposed leading edge takes on a character close to a Clark Y — blunt, forgiving, with a gentle non-snapping stall. This is a useful property for a STOL aircraft and is a direct consequence of the separation cut geometry, not an accident.
Incidence and Cruise Attitude
Wing incidence is set at +2° to the fuselage reference line (FRL). This places the wing at its best lift-to-drag AoA during cruise, with the fuselage sitting at a roughly level 2–3° nose-up attitude. The pilot sees a near-level horizon in cruise without the nose-high attitude of a high-incidence design.
Planform
Constant chord, 4 ft (1.22 m) throughout. No taper, no twist. The rectangular planform stalls root-first naturally on this section — induced downwash reaches critical AoA at the root slightly before the tip — which preserves aileron authority through the stall without requiring washout. The constant chord also simplifies rib tooling: one rib profile serves the full span.
Span: 42 ft (12.8 m)
Chord: 4 ft (1.22 m) constant
Wing area: 168 sq ft (15.6 m²)
Aspect ratio: 10.5
Spar Position
The main spar sits at the point of maximum thickness — 35% chord, or 16.8 inches aft of the leading edge. This corresponds to the rear door post on the fuselage, tying the wing's primary structural load directly into one of the fuselage's heaviest frames. The wing aerodynamic centre (25% MAC) sits 4.8 inches forward of the main spar.
Laminar Flow Intent
The 65-series section rewards a clean leading edge. The slat system necessarily disturbs the boundary layer when deployed, but at the speeds where slats are used, laminar flow is not the priority. In cruise with slats closed, the leading edge is uninterrupted and the section performs as designed.
Wing Section Design Philosophy — NACA 65(2)-415
The Amihan STOL and Amihan Glider both use the NACA 65(2)-415 aerofoil section across the full span of the shared wing. The choice of section was deliberate and is central to the modular-platform concept.
The Dual-Regime Requirement
The Amihan STOL has two distinct performance requirements that pull in opposite directions: a cruise speed of 150 knots and a STOL approach speed in the low 40s mph. Most sections optimise for one or the other. The 65(2)-415 is one of the few sections that handles both regimes cleanly, for reasons that are structural, aerodynamic and practical.
Cruise Performance
The NACA 6-series laminar-flow sections were designed specifically to maintain laminar boundary layer flow over a long run of the upper surface, minimising profile drag at a defined cruise lift coefficient. At 150 knots on the Amihan's 4ft chord, the Reynolds number is approximately 5–6 million — well within the section's design range. The laminar bucket is wide enough to hold through normal cruise attitude variation, giving genuine low-drag cruise performance rather than a theoretical one.
Low-Speed Performance
At low speed with the automatic slats deployed, the main element's leading edge is exposed as a new, blunter profile with a Clark Y character — exactly what a STOL approach needs. The slats take over the boundary layer re-energisation job that laminar flow performs at cruise. This is a clean handoff between two aerodynamic regimes: the section does not have to compromise between them because the slat system handles the transition.
Structural Suitability
At 15% thickness on the 48-inch chord, the 65(2)-415 gives a spar height of approximately 7.2 inches at the root. This is adequate for both the glider spar (solid foam-core, 8-ply UD carbon caps) and the STOL spar (hollow box-beam, 24-ply UD carbon caps) without requiring an oversize section that would penalise cruise drag.
Alternatives Considered
Three alternative sections were assessed:
-
NACA 4415 — blunter nose and more camber, better low-speed Cl-max increment from the slats, but higher profile drag at cruise. Would penalise the 150-knot cruise target. Ruled out on cruise performance grounds.
-
Wortmann FX 61-184 — excellent glider cruise at low Reynolds numbers, good low-speed behaviour, but optimised for a Re range well below the STOL's cruise condition. Would run above its design Re at 150 knots. Ruled out on cruise Reynolds number grounds.
-
Eppler E387 — outstanding low-Re glider performance but only 9% thick, giving a root spar height of approximately 4.3 inches. Structurally inadequate for either spar design, and insufficient leading-edge depth for the confirmed slat bull-nose geometry. Ruled out on structural grounds.
Pilot Familiarity
The designer has extensive PA-28-140 hours on the NACA 65(2)-415 in practice, including demonstrated STOL performance of under 300 feet in 15–20 knot wind conditions without a wing drop. The section's forgiving stall behaviour, progressive warning and honest response at the edge of the envelope are known quantities from direct experience. Since the designer will conduct all flight testing, this is a genuine safety consideration, not a secondary one. The aerodynamic character of the main element will be familiar at the point in the envelope where familiarity matters most.
Conclusion
The NACA 65(2)-415 is retained for both aircraft as the best available compromise across cruise performance, low-speed handling, structural efficiency, slat compatibility and pilot familiarity. The modular-platform concept — one wing, one set of tooling, shared rib geometry, skin moulds and root hardware between the glider and the STOL — requires a single section to serve both roles. The 65(2)-415 serves both roles without significant penalty in either direction.
---
CHAPTER 4 — HIGH-LIFT SYSTEM
Philosophy
The slat system is the heart of the Amihan's STOL performance. The investment in slat complexity pays for the docile low-speed handling and the low stall speed. Everything else in the design is kept simple.
Automatic leading-edge slats require no pilot input, no actuators, and no switches. At low angle of attack they are held closed by aerodynamic pressure. As AoA increases, a suction shift at the leading edge pulls the slat forward and down on its tracks, opening a slot that re-energises the boundary layer and delays stall. The pilot gets the benefit without managing it.
Layout
Full span, two sections per wing. Each section spans approximately 10.5 ft (half the 21 ft semi-span). The break between sections sits at the mid-span point and is faired with a wing fence.
Each section has its own independent torque tube running spanwise inside the slat body, connecting the two track stations at each end of that section. The torque tube's sole job is to keep the slat from cocking or skewing on its tracks — it carries no aerodynamic deployment load. Because the two sections are mechanically independent, each can deploy at its own rate without transmitting binding loads from one panel to the other, and each panel is self-contained for disassembly.
No differential deployment tuning between sections is needed. The constant-chord rectangular planform already stalls root-first naturally. Both slat sections deploy together and that is the correct outcome on this wing.
Track Geometry
Each slat section runs on two tracks, one at each end, mounted to structural rib stations in the leading-edge structure forward of the main spar. The track arc moves the slat simultaneously forward (opening the slot gap) and down (drooping the nose to increase effective camber) as it deploys. A straight track cannot do both cleanly; the track is therefore curved, with an arc radius of approximately 3–4 inches.
Track angle: approximately 15–20° nose-down to the chord line
Slat travel: approximately 1.5–2 inches forward, 0.8–1 inch down
Deployed droop: approximately 15–20° below the chord line
Before cutting aluminium, the arc geometry is to be verified against the foam leading-edge model. Mock up in card or thin ply, confirm the closed-position fit and deployed gap, then transfer to aluminium extrusion.
Track material: 6061-T6 aluminium extrusion (C or T section), bent to the arc radius on a bending jig.
Slot Geometry
The slot between the slat trailing edge and the new main-element leading edge is convergent — wider at the entry (leading-edge side) than at the exit (upper surface side). This accelerates the flow through the slot and re-energises the boundary layer on the main element's upper surface.
Target slot exit gap (trailing-edge gap at full deployment): 1.0–1.25 inches (approximately 2–2.5% chord). Below 1 inch the slot chokes; above 1.5–2 inches it becomes a pressure bleed rather than a controlled jet.
The slot exit should be positioned tangentially to the main element's upper surface at the new leading-edge stagnation point — the point where the boundary layer is most at risk of separating with the slat deployed. On the Amihan, this is approximately 1–2% chord of the new main element, very close to the new nose.
The slat trailing edge must be positioned forward of and slightly above the new main-element nose — not tucked behind it — so the accelerated jet attaches to the upper surface rather than dumping into the scoop cavity.
Main-Element Leading-Edge Profile
With the slat deployed, the new main-element leading edge is exposed. This begins approximately 1.25 inches aft of the original NACA nose point and curves smoothly up to rejoin the original upper camber line at approximately 5 inches aft — a slat chord of roughly 10% (4.8 inches on the 48-inch chord).
The lower termination of the separation cut ends in a rounded bull nose rather than a square cutoff. Radius approximately 0.75–1.2 inches (15–25% of slat chord). The rounded nose gives the new main-element LE a clean stagnation point at high AoA, tolerates track and fit variation in the closed position, and avoids separation at the nose when the slat is fully deployed and high-AoA inflow arrives from below. The slat's own trailing edge at the lower end is likewise rounded so the two surfaces nest cleanly when closed.
Wing Fence
A wing fence at the mid-span section break serves two purposes: it fairs the gap between the two slat sections, and it acts as an aerodynamic fence limiting spanwise boundary-layer migration and reinforcing the root-first stall progression. The fence is also a structural rib-doubler providing end support for the slat tracks at the break.
Rib Stations for Slat Attachment
Six structural rib stations per wing are required for the slat system:
- 4 track-attach ribs or doublers (one at each end of each of the two sections)
- 2 torque-tube support-bearing ribs (approximately mid-panel on each section)
These are additional to the wing's general rib spacing and must be checked against the overall rib layout plan.
Slat Specification — Confirmed from Foam Model
The following geometry is confirmed from the physical foam leading-edge model and represents the template for the aluminium track fabrication.
Slat Geometry
Slat chord: 5.3 inches (11% of the 48-inch wing chord)
Droop at full deployment: 15° below the chord line
Bull nose radius at lower termination: 7/8 inch (0.875 inch)
Slot exit gap at full deployment: 1.0 inch
Overlap (slat TE forward of new main-element LE): 0.625 inch (~1.3% chord — within the 1–2% target)
Track Arc Geometry
Arc centre: 3.0 inches aft of the new main-element LE, on the original chord line
Arc radius: 7 5/16 inches (7.3125 inches)
Arc sweep: approximately 20° at the pivot (to be confirmed with protractor)
Path length along arc: approximately 2.5 inches (closed to fully deployed)
Track Construction
Material: 6061-T6 aluminium extrusion, C-channel section
Wall thickness: 1/8 inch
Slot length: approximately 3.0–3.25 inches (2.5 inches travel plus end clearance)
Rollers: two per track (one at each end of the slat), 3/8 or 1/2 inch diameter, running inside the C-channel
Channel opening: approximately 1/2–5/8 inch (roller diameter plus running clearance)
Track Mounting
Track stations: two per slat section — one at each end
Arc centre location on rib: 3.0 inches aft of the new main-element LE on the original chord line — this point is the reference for locating the track on every rib station along the span
Torque tube: one per slat section, running spanwise inside the slat body, connecting both track stations. Purpose is anti-skew only — keeps the slat from cocking on its tracks. Carries no aerodynamic deployment load.
Notes
The 20° arc sweep and 15° deployed droop are different quantities measuring different things: 20° is how far the contact point travels around the arc centre; 15° is the net angular attitude change of the slat itself. The difference is accounted for by the forward translation component of the slat's travel along the arc.
The arc sweep of 20° is a foam-model estimate pending protractor confirmation. All other figures above are measured values from the physical model.
The closed-position fit must be verified before cutting aluminium track — the slat must seat flush against the new main-element LE with no aerodynamic gap in cruise. Any gap at cruise speed is a significant drag penalty at 150 knots.
Flap Slot Geometry — Confirmed
The flap slot dimensions are sized against the flap chord (12in), not the main element chord (48in), since the flap is the lifting surface being re-energised by the slot jet. The slat slot uses the main element chord as its reference — these are two different surfaces and the slot sizing follows accordingly.
Slot Gap
Target gap (measured perpendicular to the flap surface at the LE): 0.25–0.40in
This is 2–3% of the 12in flap chord
Below 0.25in the slot chokes; above 0.40in it becomes a pressure bleed rather than a controlled accelerating jet
Overlap
Target overlap: 0.75–1.0in
This lands the slot jet at approximately 6–8% of flap chord — well forward on the flap upper surface, where boundary layer re-energisation is needed
Overlap is sized against wing chord (1.5–2% of 48in), consistent with the slat overlap target
Notes
The circular flap LE radius (to be confirmed) must be sized to give a gap in the 0.25–0.40in range at full Stage 1 translation. The 1.0–1.25in gap carried over from the slat analysis does not apply here.
Production Fowler flaps consistently use a narrow slot relative to flap chord for the same reason — the flap boundary layer is short and does not need a large jet to re-energise it effectively.
CHAPTER 5 — TAIL DESIGN
Configuration
Conventional tail with a fin, rudder, and fuselage-mounted stabilator. The stabilator is a full-flying horizontal tail surface trimmed via an anti-servo tab. There is no fixed tailplane — the entire surface moves.
The stabilator is mounted low on the aft fuselage, as far below the wing wake as practical. This keeps it out of the high-AoA wake and avoids the deep-stall risk associated with T-tail configurations where the tail enters the wing wake and loses effectiveness at high angle of attack.
Fuselage Length and Moment Arm
Fuselage length: 22 ft (6.7 m)
Wing AC to stabilator hinge line: approximately 12 ft (3.66 m)
A 20 ft fuselage was considered first. At that length the moment arm is only ~10 ft, which leaves insufficient pitch authority margin when full flaps are deployed — the increased downwash from the flaps consumes most of the stabilator's nose-up trim range. Adding 2 ft grows the moment arm to ~12 ft, allows a smaller and lighter stabilator, and keeps full-flap authority comfortable without extending the trim range.
Stabilator Sizing
Tail volume coefficient target: V_H = 0.40 (consistent with Helio Courier ~0.40, Cessna 185 ~0.42)
At 12 ft moment arm and 168 sq ft wing area with 4 ft MAC:
Stabilator area: approximately 22 sq ft
Stabilator span: approximately 9.4 ft at aspect ratio 4
Stabilator chord: approximately 2.34 ft
Incidence and Trim
Stabilator neutral position: −1.5° to FRL
Trim range: ±5° via anti-servo tab
The −1.5° neutral position accounts for the wing's nose-down pitching moment (Cm₀ of the cambered 65(2)-415 section) and the approximately 1.6° of downwash at the tail in clean cruise. Decalage (wing incidence to stabilator neutral) is approximately 3.5°.
At full flap deployment, downwash at the tail increases by approximately 2–4° above the clean-cruise value. This is why the 12 ft moment arm and the low stabilator position are important — at 10 ft the increased downwash would consume the majority of the ±5° nose-up trim authority in the flare. At 12 ft the margin is comfortable.
The anti-servo tab moves in the same direction as the stabilator (unlike an anti-balance tab), providing a stick force that increases with deflection. This gives the pilot natural feel and prevents over-controlling the all-flying surface.
Thrust Line and Downwash Interaction
The UL Power 520iS drives a large, slow-turning propeller. At STOL speeds and high power settings, the propeller slipstream accelerates flow over the inboard wing and increases downwash at the tail beyond the clean aerodynamic value. This effect is most pronounced in the low-speed, high-power regime — exactly the STOL approach and go-around condition.
The low stabilator position and the ±5° trim range are both sized with this in mind. If in-flight testing reveals insufficient nose-up authority in the full-power, full-flap condition, the first corrective action is extending the trim range to ±7° before considering geometry changes.
Fin and Rudder
Fin and rudder sizing to be completed once fuselage cross-section and undercarriage configuration are finalised. The 22 ft fuselage length provides a useful fin moment arm. The longer moment arm (vs. 20 ft) may allow a slightly smaller fin for the same directional stability, partially offsetting the small weight penalty of the longer fuselage.
---
CHAPTER — TAIL DESIGN (GLIDER)
Fuselage Layout and Moment Arm
The Amihan glider fuselage is 20 ft long. The pilot sits semi-reclined with feet near the nose cone and head just below the wing leading edge, putting the seat approximately 4 ft aft of the nose. With only 4 ft of nose ahead of the wing leading edge, the wing aerodynamic centre (at 25% chord) sits approximately 5 ft aft of the nose tip.
This places the tail moment arm — wing AC to stabilator hinge line — at approximately 15 ft. That is longer than the STOL's 12 ft arm despite the same fuselage length, because the glider's short nose moves the wing well forward. The short nose, which might seem like a liability, is actually working in the design's favour at the tail.
Stabilator Sizing
Target tail volume coefficient: V̄h = 0.38 — consistent with previous analysis and appropriate for a foot-launch glider with full-span slats and Fowler flaps to 25°.
Solving for stabilator area:
Sh = (V̄h × Sw × c̄) / Lh = (0.38 × 168 × 4) / 15 = 17 sq ft
At 10% of wing area this is on the light side of the normal 13–15% range. A working target of 19–20 sq ft is adopted to preserve authority margin, particularly in full-flap approach with changing downwash. This is still noticeably smaller and lighter than the STOL stabilator at ~22 sq ft.
Moment arm (wing AC to stabilator): ~15 ft
Target V̄h: 0.38
Stabilator area: 19–20 sq ft
Span (AR 4): 8.7–9.0 ft
Chord: 2.1–2.3 ft
Estimated weight (foam/glass): 7–8 lb
Flap Authority — Why 25° is the Right Cap
At 25° flap the additional nose-down pitching moment is ΔCm ≈ −0.15 to −0.20. The stabilator's restoring authority at V̄h = 0.38 and CLh = 1.0 is ΔCm_tail = 0.38 — roughly double the flap-induced moment, leaving comfortable margin for flare and trim. This is the same conclusion reached for the STOL: 25° is the practical maximum for this tail geometry. 40° flap would drive the stabilator to 27+ sq ft and consume most of the trim authority.
The full high-lift system — automatic slats plus flaps at 10°/25° — is retained on the glider. Stall protection via active slats is more important here than on the powered STOL, since there is no engine to assist recovery in slow beach soaring. The 10° takeoff setting assists foot-launch, and 25° gives a useful approach-speed reduction and steeper glide path for landing in confined beach areas.
Pilot CG and Weight and Balance
Pilot position: semi-reclined, feet near the nose cone, hips approximately at the wing leading edge, head just below it. Pilot CG falls at approximately 2 ft aft of the nose — 3 ft ahead of the wing aerodynamic centre.
At a design pilot weight of 170 lb, the nose-down moment from pilot CG offset is:
170 lb × 3 ft = 510 ft-lb
The stabilator must carry an upload of 510 / 15 = 34 lb to trim this in level flight. At 19 sq ft stabilator area that is approximately 1.8 lb/sq ft — a very modest lift requirement, well within the surface's range. The trim condition is a small upload, meaning the aircraft has a natural nose-down (stable) tendency in pitch. This is correct.
Pilot weight range is 140–200 lb. The resulting CG moment swing is ±90 ft-lb around the design value — from 420 ft-lb at 140 lb to 600 ft-lb at 200 lb. Both extremes are within the anti-servo tab trim authority and require no ballast or geometry changes.
Structural Note
The spar carry-through sits at the wing leading edge, coinciding with the pilot's hip/seat location. This places the wing's heaviest structural member adjacent to the heaviest pilot mass, minimising fuselage bending load along the belly. The nose section forward of the feet is essentially a fairing — minimal structure, minimal weight, no ballast required.
Fin and Rudder
Fin and rudder sizing to be completed once fuselage cross-section is finalised. The 15 ft tail moment arm provides useful directional authority from a modest fin area. Sizing will follow the same tail volume approach used for the stabilator, targeting a vertical tail volume coefficient in the range of 0.02–0.025, consistent with a single-seat foot-launch glider with spoileron roll/yaw coupling reducing the rudder's adverse-yaw workload.
CHAPTER 6 — POWERPLANT AND THRUST LINE
Engine
UL Power 520iS
Power: 200 hp
Configuration: air-cooled, horizontally-opposed six-cylinder, fuel-injected
Dry weight: approximately 185 lb
This engine is purpose-built for experimental and light sport aircraft. It is fuel-injected (no carburettor icing), air-cooled (no coolant system weight or plumbing), and has a proven track record in the STOL and bush-flying community.
Thrust Line
Right offset: 2°
Down thrust: 3°
The right offset counters the left-turning tendencies at high power (propeller torque, P-factor, gyroscopic precession, and spiralling slipstream). The down thrust counters the pitch-up moment that occurs when power is increased at low speed — without it, the pilot must push forward on the stick every time power is added in the approach or go-around.
The 3° down thrust is slightly more aggressive than the Cessna 185's 2–3°, reflecting the 520iS's large, slow-turning propeller which generates stronger P-factor effects at the high angles of attack typical of STOL operations.
These offsets mean the aircraft flies essentially hands-off at cruise power and cruise attitude. At full power in the climb, a small amount of right rudder is still required — this is normal and expected.
Fuel System
Fuel type: automotive gasoline (mogas) or aviation gasoline (avgas) — the 520iS is certified for both
Tank location: single fuselage tank, mounted behind the seats
Capacity: 50 US gallons usable
Fuel weight: approximately 300 lb at full tanks (50 × 6 lb/USG)
Endurance: approximately 6.25 hours at 75% cruise power (8 GPH)
Range: approximately 625–650 nm at 150 knots with reserves
CG Effect of Fuel Burn
The fuel tank sits behind the seats, aft of the wing aerodynamic centre. As fuel burns, the CG moves forward — toward the forward limit, not away from it. This is the stable direction for fuel burn: the aircraft becomes progressively more nose-heavy as the flight progresses, which is manageable with trim and is preferable to an aft CG shift as fuel depletes.
Full fuel (300 lb aft of CG): most critical aft CG condition — check against 33% MAC limit
Half fuel (150 lb): near-neutral CG effect
Reserves only (~15 lb): most critical forward CG condition — check against 15% MAC limit
The fully-loaded aft CG case (two crew, full fuel, full baggage) and the light forward case (solo pilot, minimum fuel) must both sit within the 15%–33% MAC envelope. Preliminary W&B calculations confirm both cases are within limits with the current component layout. These should be rerun once real component weights are available.
Power Loading
Gross weight 1,440 lb / 200 hp = 7.2 lb/hp
This is comparable to the Helio Courier (~8 lb/hp) and is consistent with strong STOL climb performance and a useful reserve of power for go-arounds in the float configuration.
CHAPTER 7 — WEIGHT AND BALANCE
Datum
The firewall is used as the CG datum (0 inches). All moments are measured in inches aft of the firewall. Negative values are forward of the firewall (engine, propeller).
CG Envelope
Wing aerodynamic centre: 25% MAC = 53.2 inches aft of firewall
Forward CG limit: 15% MAC = 48.2 inches aft of firewall
Design CG target: 25% MAC = 53.2 inches aft of firewall
Aft CG limit: 33% MAC = 56.8 inches aft of firewall
The envelope is deliberately narrow in the aft direction. The stabilator has authority well beyond the 33% limit, but handling qualities degrade progressively aft of that point and the limit is set conservatively.
Component Table
| Component | Weight (lb) | Arm (in aft of FW) | Moment (lb·in) |
|---|---|---|---|
| Engine (UL Power 520iS) | 185 | −24 | −4,440 |
| Propeller | 15 | −36 | −540 |
| Fuel (full, 50 USG) | 300 | ~62 | 18,600 |
| Fuel (reserves, ~15 lb) | 15 | ~62 | 930 |
| Two crew (2 × 170 lb) | 340 | ~22 | 7,480 |
| Baggage | 100 | ~50 | 5,000 |
| Airframe/systems (placeholder) | 500 | ~36 | 18,000 |
Note: Airframe/systems figure is a placeholder. Wing structure, fuselage, tail, undercarriage, and systems weights must be itemised once component design is further advanced.
Loaded CG Cases
Worst-case aft (full fuel, two crew, full baggage):
Total weight ~1,440 lb, CG approximately 44 inches aft of firewall — well within the 56.8 inch aft limit.
Worst-case forward (reserves only, two crew, no baggage):
Total weight ~1,055 lb, CG approximately 33 inches aft of firewall — within the 48.2 inch forward limit.
The heavy engine sitting well forward of the firewall pulls the CG forward in both cases, providing comfortable margin against the aft limit and keeping the forward case within bounds even at minimum fuel.
Fuel Burn and CG Movement
As fuel burns from the aft tank, CG moves forward. The aircraft becomes progressively more nose-heavy through the flight. This is the stable direction — trim adjustment is required but the tendency is toward greater stability, not less. No fuel management procedure is required to maintain CG within limits during normal operations.
Notes for Refinement
The component table should be rerun with real weights once the following are confirmed:
- Wing structure (spar, ribs, skin, slat system)
- Fuselage structure (frames, skin, carry-through beam)
- Tail assembly (stabilator, fin, rudder, control runs)
- Undercarriage (wheels and floats, if both are to be carried)
- Engine installation (mount, exhaust, cooling baffles)
- Avionics and electrical system
- BRS parachute system (if installed — approximately 25–30 lb, attachment points forward at firewall frame and aft at baggage bulkhead)
The BRS attachment points should be designed into the fuselage frame now as primary structure, before the fuselage layout is finalised, rather than retrofitted later.
---
CHAPTER 8 — STRUCTURAL DESIGN
Design Philosophy
The Amihan STOL is designed to 2,000 lb gross weight at utility category load factors (+3.8G / −1.5G limit, +5.7G / −2.25G ultimate) while targeting a 1,200–1,440 lb operating weight. The structural margin this provides means the airframe has room to grow — additional equipment, float installation, or a heavier powerplant — without requiring a structural redesign.
All composite-to-metal joints use bonded aluminium or steel fittings with mechanical fastener backup. The bond carries distributed shear; the fasteners carry peel and serve as a secondary load path if the bond is ever compromised. The pin always passes through metal, never through composite directly.
Wing Spar — STOL
The powered spar is a hollow box beam with carbon fibre caps and a multi-panel foam-core web.
Caps:
Fibre: unidirectional carbon tape, T700-equivalent, 200 g/m²
Root layup: 24 plies, approximately 9.6 mm thick
Taper: ply drops following the bending moment curve, scarfed at 1:50–1:100, staggered 25–50 mm apart, no more than two plies dropped at any one station, at least one ply continuous tip to root
Cap width: 3 inches (76 mm), constant
Outer face: full-span plies laid on the tool face, giving a constant spar depth reference along the span and a tool-quality bond surface for the skin
Inner face: tapered/dropped plies laid against the web
Web:
Six panels of 0.5-inch Divinycell H80 foam core, each skinned in 200 g/m² ±45° biaxial carbon on both faces
Panels built in three pairs, each pair pre-cured and inspected before being bonded together with Plexus methacrylate adhesive
Foam joints between pairs staggered by half a core length for structural continuity
Web assembly: 3 inches thick × approximately 7 inches deep × 21 ft span
Root plug: solid carbon laminate (no foam) over the last 8–10 inches of each web panel where the root fitting bears. Foam-to-solid transition scarfed over 2–3 inches — no square-edge step
Post-cure:
Caps post-cured at 60°C / 140°F for a minimum of 2–4 hours after full room-temperature cure. Start the post-cure clock only when the part centre reaches temperature (thermocouple recommended). Support flat throughout.
Web panels post-cured with H80 core in place — Divinycell H80 is rated to approximately 80°C, safely above the 60°C post-cure temperature. Stack web panels with spacers between them during post-cure to allow airflow to the centre panels.
Spar Cap Mould and Post-Cure Procedure
Mould Construction
The spar cap mould is a 21-ft aluminium tooling plate, 6061-T6, 1/2-inch thick. The top face is the tool surface — flat, smooth, and used as the reference for the finished cap. The bottom face carries the heating system.
Silicone heat tape is bonded to the underside of the plate in a serpentine pattern, 3–4 inches between runs, running the full 21-ft length. For a 3-inch wide cap, one run of 1-inch tape centred under the cap width is sufficient — the aluminium spreads heat laterally before it reaches the part. Total heat tape output for a 21-ft run at 6–10 W/ft is approximately 125–210W, well within a standard 15A circuit. If the tape's rated length requires it, split into two 10.5-ft circuits on the same PID controller with two relay outputs.
One inch of rigid polyiso foam board, foil-faced, is bonded to the entire underside below the heat tape. This keeps heat moving upward into the tool and prevents heat loss into the bench.
Vacuum seal rails run along both long edges of the plate — either a 1-inch wide × 1/8-inch deep rebate machined into the top face along each edge, or aluminium angle bonded to the underside so the top plate face is the only sealing surface. Without positive seal rails the vacuum bag bridges the plate edge and leaks.
Temperature control is a PID controller with a thermocouple bonded to the tool surface at mid-span, alongside the cap (not under it). The PID drives a relay output to the heat tape circuits. Set point 80°C for OOA prepreg cure; the same tool post-cures wet layup at 60°C.
Material — Out-of-Autoclave Prepreg
The cap is laid up in T700 unidirectional OOA prepreg tape, 200 g/m², on this tool rather than dry fabric with infusion. OOA prepregs (Toray TC250, Cytec MTM45-1, or similar) cure at 80°C under vacuum bag only — no autoclave required. This gives a controlled fibre volume fraction of 55–60% without the resin metering and flow-path management of infusion, and eliminates the risk of a dry spot at mid-span on a 21-ft part.
Prepreg must be stored at −18°C in a dedicated chest freezer. Track cumulative out-time from first removal — most OOA systems allow 30 days out-time before tack and flow properties degrade. A full spar cap layup consumes 2–3 days of out-time at most.
Layup Procedure
Prepare the tool surface: abrade lightly with 120-grit, blow clean, apply mould release. Lay peel ply on the tool face — this becomes the bond face of the cap to the spar web.
Lay 24 plies of UD prepreg tape, outer plies first (these go down onto the tool face and become the outer face of the cap). All fibres run spanwise, 0° to the spar axis. Each ply is rolled down firmly with a rubber roller to consolidate tack and remove air. Ply drops follow the bending moment curve: no more than two plies dropped at any one station, drops staggered 25–50mm apart, scarf ratio 1:50–1:100, at least one ply running continuous tip to root.
Apply peel ply to the top face of the layup. Apply perforated release film. Apply breather fabric — run it continuously end to end, from one tip to the other, with the vacuum port at mid-span. A break in the breather leaves a section of bag unsupported without a vacuum indicator. Apply vacuum bag film and seal to the tooling plate with tacky tape against the seal rails. Pull vacuum to full (−14.5 psi or better), check for leaks, and hold bag vacuum for 30 minutes before beginning the cure ramp.
Cure and Post-Cure
Ramp temperature at 1–2°C per minute to 80°C. A fast ramp can cause outgassing in a partially gelled laminate — the PID ramp-rate function handles this if available; otherwise dial the setpoint up in 10°C steps every 5 minutes. Hold at 80°C for 2 hours minimum under full vacuum. Allow the tool to cool below 40°C before releasing vacuum and removing the part.
The vacuum bag, breather, and release film are single-use consumables — replace for any further post-cure cycles.
The cap comes off the tool with a tool-quality outer face. The peel ply is stripped immediately before any secondary bonding to the spar web — peel-plied surfaces must be bonded within 4–8 hours of stripping; if that window is missed, abrade lightly with 80-grit and degrease with IPA before bonding.
Dimensional Check
With the cap still on the tool (before vacuum bag removal), measure flatness along the full 21-ft span using a straightedge or laser level. Any bow greater than 1/8 inch over the span length should be investigated — it indicates either a temperature gradient along the tool or bag bridging at a mid-span point. A thermocouple at each end of the tool in addition to the mid-span control thermocouple helps identify gradients on a long part.
Wing Spar — Glider
The glider spar is a solid foam-core wrapped spar — the construction method validated by the 1,000 Pound Beam Challenge.
Caps: unidirectional carbon or glass, 8 plies / approximately 3.2 mm at root, tapering to tip
Web: ±45° biaxial glass over foam core
Root fitting: machined 7075-T6 aluminium, single-piece, inverted-U profile
The solid core is chosen specifically because it handles the stress riser at the stub-socket joint much better than a hollow box beam. The foam prevents the abrupt inner-surface stress concentration that would occur in a hollow section at that location.
Root Fitting — STOL
Material: fabricated 4130 chromoly steel, TIG-welded, coated for corrosion protection
Profile: inverted-U — a top plate bonded to the cap's upper face, with two web legs dropping down on each side of the spar web, terminating at the cap/web junction
Lug: a separately machined 4130 pad welded to the web leg, bored and reamed for the wing pin after welding (weld first, machine last to correct for distortion)
Pin centreline: at the cap mid-thickness, so the pin load transfers with no eccentricity into the cap's axial force
Bonding: Plexus MA550 to both the cap top face and the web leg faces, surface prep per Plexus protocol (80-grit abrade + IPA degrease + MA1000 primer on the steel)
Clamping bolts: AN5 (5/16"–24 UNF) through the cap top, torqued to 100–140 in-lb, engaging steel tapped backing plates bonded and recessed into the solid web piece
Perimeter seal: marine-grade sealant around the full fitting perimeter after bonding — the aluminium/steel-to-carbon interface edge is a moisture ingress path in a saltwater environment and must be sealed
Root Fitting — Glider
Material: machined 7075-T6 aluminium billet, single piece (top plate, web legs, and lug in one part — no welding required at glider-spar load levels)
Same bonding and bolt protocol as the STOL fitting
Pin: same 5/8-inch 4130 steel wing pin, torqued to approximately 57 ft-lb as a friction-grip joint
At glider load levels (~12,000–15,000 lb pin load vs. ~100,000 lb for the STOL), the hardware is operating at a fraction of its rated capacity
Wing Attachment Pin
Diameter: 5/8 inch
Material: 4130 steel
Torque: approximately 57 ft-lb (friction-grip / slip-critical joint)
Joint type: double shear — fuselage carry-through ears straddling the spar root lug
The clamped faces carry shear by friction before the pin shank sees any bearing load. The pin is sized primarily for the clamp-load requirement, not shear alone.
Both the glider and STOL spars use identical pin geometry — the carry-through hardware never changes between aircraft versions.
Leading-Edge Tang
The D-nose torsion box (skin and spanwise stringers forward of the main spar) extends inboard through the root rib and protrudes into the fuselage as a tang, carrying drag and torsional loads separately from the main spar pins.
The tang is not a discrete bolted-on fitting — the spanwise unidirectional stringers converge and terminate into a short machined aluminium fitting at the root, with the D-nose skin tapering in alongside. The tang pin passes through the metal fitting only. This is the same bonded-metal-fitting principle as the root spar fitting: fibres terminate gradually into the fitting, the fitting takes the pin load, composite never sees pin bearing stress directly.
The tang effectively replaces the need for a separate leading-edge alignment pin — it self-locates the wing in chord and carries the drag/torsion load in one piece of structure.
Assembly sequence: the tang drops into a pocket in the fuselage frame forward of the carry-through beam as part of wing alignment, tang pin is inserted first (wing now located in drag and torsion), then upper spar pin, then lower spar pin. Wing removal is the reverse: lower pin, upper pin, tang pin, lift clear.
Carry-Through Beam
Short aluminium box-beam or I-section spanning the 43-inch cabin width at the roof level, with steel lug ears at each end engaging the spar root lugs. The carry-through does not intrude into the cabin — it sits above it, accessed via an inspection panel in the wing-root fairing.
Both spar versions (glider and STOL) share identical root lug geometry: same pin centreline height, same pin diameter, same lug plate geometry, same carry-through end fittings. Swapping between aircraft is a matter of disconnecting controls and wiring at the root, pulling three pins, and lifting the wing clear.
Ribs
Cored composite construction with double-L flanges at the spar slot — one flange bonding to the cap face, one to the web face — spreading the air-load shear transfer over area rather than relying on a butt bond at the slot edge alone.
Rib slots are sized to the local spar depth at each span station (the cap tapers, so the slot must match). Each rib sits perpendicular to the spar axis.
The root rib is built substantially heavier than the general ribs — glass or carbon, not foam-cored — as it carries the tang loads and the concentrated spar/D-nose transition forces.
Stringers run continuous through all rib bays, bonding well at each rib station. A broken stringer bond at a rib creates a local stress concentration rather than a smooth load transfer — continuity is essential.
Skin and Stringers
Moulded carbon skins, upper and lower. The D-nose skin forward of the spar closes with the spar web to form a closed torsion box — the primary torsional stiffness element of the wing. The rear skin closes the section aft of the spar.
Stringers and skin carry approximately 15–30% of total bending stiffness in addition to torsion and shear — the spar sizing is therefore conservative in practice, since it is calculated as if the spar carries bending alone.
Build sequence:
1. Build and post-cure the main spar (caps and web panels separately, then assembled)
2. Bond root fittings and nut plates to the fully cured spar using a root alignment fixture
3. Slide cored ribs onto the spar and bond in place
4. Bond spanwise stringers into the rib stations using a jig template for consistent spacing
5. Bond the D-nose tang fitting into the root rib / stringer termination
6. Bond the spar/rib/stringer lattice onto the lower moulded skin
7. Bond the upper skin to close the section
The upper skin closure bond is the most critical and least inspectable joint in the wing. Use fresh-abraded / peel-plied bond faces on both sides. A wet-laid or co-cured upper skin gives a stronger bond than a secondary bond to a pre-cured skin.
Wing Skins — Material and Fabric Selection
The upper and lower wing skins are moulded biaxial carbon prepreg, laid up in female
moulds made from plugs built to the NACA 65(2)-415 profile. The plug-and-mould route
is chosen because it gives a tool-quality outer surface — critical for maintaining
laminar flow over the 65-series section in cruise — and because the female mould
becomes the post-cure fixture, holding the skin to the correct airfoil geometry
throughout the cure cycle.
Fabric Selection — Biaxial ±45°, Not Triaxial
The skins are biaxial carbon at ±45° to the span axis. This is the structurally
correct choice for a spar-built wing and is worth stating explicitly, because triaxial
(0°/±45°) cloth is sometimes assumed to be superior on account of having more fibre
directions. For this application it is not.
The wing skin on a spar-built aircraft has two structural jobs: carry torsion, and
maintain the airfoil shape against panel buckling. It does not carry the primary
spanwise bending load — that is the spar's job. The ±45° fibres are almost perfectly
oriented for torsional shear, which is the skin's primary load. Adding 0° fibres
(as in triaxial cloth) would introduce fibres oriented along the span that are
redundant for torsion and create a parallel bending load path alongside the spar
caps — a path that has not been designed for and whose load sharing cannot easily
be quantified.
Biaxial ±45° keeps the load paths clean: bending in the spar caps, torsion in the
skins. Triaxial would blur that separation without improving torsional performance
and at the cost of additional weight and reduced drapeability over the curved
leading edge.
Where triaxial makes sense is a monocoque or stressed-skin design where the skin
itself must carry both bending and torsion with no discrete spar. That is not this
aircraft.
Layup Schedule
Standard laminate: two plies of biaxial prepreg per skin panel, giving a finished
skin thickness of approximately 0.4–0.6 mm. A third ply is added inboard where
torsional loads are higher, tapering to two plies outboard. The constant-chord
planform means the torsional load per unit span increases toward the root as the
accumulated torque from the full semi-span builds up — the inboard skin reinforcement
follows this gradient.
If panel buckling analysis indicates the flat aft section of the airfoil (aft of the
main spar) is marginal, the answer is a foam sandwich core in that region, not
additional ±45° plies. A foam core increases buckling resistance far more efficiently
per unit weight than additional skin laminate.
Post-Cure in the Mould
The skins are cured and post-cured in the female mould under vacuum, before
demolding. This is not optional for biaxial carbon — it is the step that locks the
correct airfoil geometry into the part.
A thin biaxial carbon skin is springy. When released from the mould it will spring
back slightly from the tool surface due to the anisotropic thermal and cure shrinkage
of the laminate — a phenomenon called spring-in. If the skin is demolded before
post-curing, the spring-in shape is what gets locked in permanently. If it is
post-cured in the mould under vacuum, the mould surface holds the skin to the
correct profile while the resin cross-links fully. Spring-in is not eliminated but
it is minimised and, more importantly, it is consistent part to part.
The cure sequence is:
1. Lay biaxial prepreg into the waxed female mould.
2. Apply peel ply, perforated release film, breather, and vacuum bag. Seal to the
mould flange with tacky tape.
3. Pull full vacuum and hold for 30 minutes to check for leaks.
4. Ramp temperature at 1–2°C per minute to 80°C. PID controller reading a thermocouple
on the mould back-face — not in the shop air.
5. Hold at 80°C for a minimum of 2 hours under full vacuum. For OOA prepreg cured
correctly at 80°C, this is both cure and post-cure in a single cycle — no separate
post-cure step is required.
6. Cool to below 40°C before releasing vacuum or opening the bag.
7. Demold. The skin comes off the tool fully cured and geometrically stable.
Mould Heating
Each skin mould (top and bottom, one per wing semi-span, four moulds total) is
heated by silicone resistance tape bonded to the back face of the mould shell in a
serpentine pattern, backed with rigid polyiso foam insulation board to direct heat
into the mould rather than into the shop air. This is the same approach used for
the spar cap mould, scaled to a larger curved surface.
Required heating power for a 60–70 sq ft mould half at 80°C in a temperate shop:
approximately 1,000–1,500 W per mould. This is achievable with two or three runs
of 500 W silicone heat tape, or equivalent area of tooling-grade radiant tape at
200–300 W/m². A PID controller reads a thermocouple bonded to the mould surface
at the coldest point (typically the perimeter) and drives relay-switched circuits.
Setting the thermocouple at the coldest point — not the warmest — guarantees the
entire skin reaches cure temperature, not just the centre.
The mould shell requires a flat sealing flange, minimum 2–3 inches wide, running
continuously around the full perimeter of the airfoil cavity. This is the vacuum
bag seal surface. It must be designed into the plug and built into the mould — a
mould without adequate seal flanges produces chronic bag leaks at the perimeter
and uneven vacuum across the skin.
Spring-In — Test Before Committing the Plug
Spring-in for biaxial carbon skins on a moderately cambered airfoil is typically
0.5–1.5° per curved section. For a 4 ft chord wing with the curvature of the NACA
65(2)-415, this is small in absolute terms but measurable. If the finished skin is
required to sit precisely on the upper surface of the rib set, the plug can be
built slightly over-cambered to compensate — the moulded skin then springs in to
the correct geometry on demolding.
The compensation is an empirical number, not a calculated one. Before cutting the
full-size plugs, build a small test section — approximately 12 inches span, full
chord — from the actual prepreg material and the actual layup schedule. Cure and
demold it, measure the spring-in, and adjust the plug geometry accordingly. This
is a half-day of work that removes the main geometric uncertainty from the full
plug build.
CHAPTER 9 — ASSEMBLY AND MODULARITY
The Modular Platform Concept
The Amihan wing is designed to serve two aircraft from one set of tooling. The glider spar and the STOL spar are different structural components — different layup schedules, different root fitting materials — but they share identical external geometry: same chord, same span, same rib profile, same skin moulds, same root pin positions, same carry-through hardware.
The fuselage side of the joint never changes. The carry-through beam, the lug ears, the tang pocket, and the pin hardware are identical regardless of which spar is fitted. This is the constraint that makes the platform genuinely modular rather than merely similar.
Wing Attachment — Three Pins
Each wing attaches to the fuselage at three points:
Tang pin — passes through the leading-edge tang fitting into a pocket in the fuselage frame forward of the carry-through beam. Reacts drag loads and torsional loads (as a couple with the main spar pins). Inserted first during assembly, removed last during disassembly. Self-locates the wing in chord and fore-aft position.
Upper spar pin — passes through the upper carry-through ear and the upper spar root lug in double shear. Reacts the bending moment as a compression force in the upper cap. Inserted second.
Lower spar pin — passes through the lower carry-through ear and the lower spar root lug in double shear. Reacts the bending moment as a tension force in the lower cap. Inserted third.
All three pins are 5/8-inch 4130 steel, torqued as friction-grip joints. All three pull out in the same direction — outboard to inboard — so wing removal requires access from one side only.
Wing Removal Sequence
1. Disconnect flying controls at the root (aileron and slat connections)
2. Disconnect electrical connections (lighting, instrumentation if applicable)
3. Remove lower spar pin
4. Remove upper spar pin
5. Remove tang pin
6. Lift wing clear
Assembly is the reverse. The tang self-locates the wing before any structural pins are inserted, so the upper and lower spar pin holes are already aligned when the tang pin goes in. No jacking or special alignment tools are required for normal assembly.
Trailer Configuration
Each wing panel is approximately 21 ft long as a single piece. With the wings removed, the fuselage is 22 ft long. A trailer of approximately 22–23 ft accommodates the fuselage; the wing panels travel alongside or above it.
No mid-span break is required. Root-only disassembly gives two panels per aircraft, four attachment points total, and a straightforward trailer load without the complexity of a mid-span joint.
Shared Tooling
The following items are identical between the glider and STOL builds and are made once:
- Rib profile and rib mould (constant chord, one profile)
- Upper and lower skin moulds (same planform, same section)
- Root alignment fixture (sets pin hole positions relative to spar outer face)
- Slat track jig (same chord, same LE geometry)
- Wing assembly jig (sets dihedral, incidence, and sweep — all zero or nominal)
The root alignment fixture is the most critical shared tool. It holds the upper lug, lower lug, and tang pin hole positions to the correct relative geometry during fitting installation, regardless of minor construction variation between individual spars. Both spars must present identical pin hole positions to the carry-through — the fixture enforces this.
Slat System Assembly
Each slat section is self-contained: two track stations, one torque tube, two sets of roller blocks or slider carriages. The section assembles to the wing before the upper skin is closed, with track attach ribs already in place. The torque tube connects to bellcranks at each track station, converting rotation into linear slat travel.
At the mid-span wing fence, the two sections are mechanically independent. The fence fairs the gap and provides end-bearing support for the inboard track of the outboard section and the outboard track of the inboard section. Each section can be removed independently for inspection or repair without disturbing the other.
Control Connections at the Root
Aileron control: push-pull tube or torque tube, disconnecting at a clevis or splined coupling at the root rib. Quick-disconnect preferred — the connection should be completable by one person without tools.
Slat system: aerodynamically automatic, no control runs. No connection required at the root for the slat.
Flap system (if fitted): to be determined when flap configuration is finalised. A simple pivot-and-pushrod disconnect at the root rib is the target.
Float Installation
Float attachment points are to be designed into the lower fuselage structure from the outset — four hard points, one per float strut, with load-spreading doublers built into the fuselage frames. Retrofitting float attach points to a finished fuselage is structurally and practically difficult; designing them in from the beginning costs almost nothing.
The BRS parachute harness attachment points (two forward at the firewall frame, two aft at the baggage bulkhead) should likewise be built into the primary fuselage structure now.
---
CHAPTER 10 — PERFORMANCE TARGETS
Stall Speed
Amihan Glider: 31 mph clean, lower with slats deployed
Amihan STOL: low 40s mph clean, meaningfully lower with slats and flaps deployed
The STOL stall speed target is set by the operating environment — short beaches, sheltered coves, gravel bars — where approach speeds must be low enough to stop in the available distance. The automatic slat system and the docile Clark-Y character of the main element under the slat are the primary means of achieving this.
Cruise Speed
Amihan STOL: 150 knots true airspeed at 75% power
Amihan Glider: not applicable (unpowered)
The 150-knot cruise target requires the slats to seat cleanly in the closed position with no aerodynamic gap in cruise — any gap is a significant drag penalty at this speed. The closed-position fit of the slat against the new leading edge must be verified on the foam model and confirmed in early flight testing.
Climb Performance
Power loading of 7.2 lb/hp (at 1,440 lb gross) is comparable to the Helio Courier and consistent with a useful climb rate in the 800–1,000 ft/min range at sea level, degrading gracefully at altitude. Specific climb rate to be calculated once propeller selection is finalised.
Glide Ratio
Amihan Glider target: approximately 30:1
Achievable for a clean 42 ft laminar wing at 385 lb gross weight. The slat system will disrupt laminar flow when deployed, but at the speeds where slats are needed the glider is flying slowly enough that laminar flow is not the priority. In clean cruise configuration with slats sealed, the 65(2)-415 section performs as designed.
Range and Endurance — STOL
Fuel capacity: 50 US gallons usable
Cruise fuel burn: approximately 8 GPH at 75% power
Endurance: approximately 6.25 hours with reserves
Range: approximately 625–650 nm at 150 knots with reserves
Power Loading
1,440 lb gross / 200 hp = 7.2 lb/hp
This figure will improve as the empty weight estimate is refined downward from the current 700 lb placeholder. A 650 lb empty weight at the same gross gives 7.2 lb/hp unchanged (gross weight drives power loading, not empty weight directly), but the useful load improves and the aircraft's performance margins widen.
Undercarriage
Wheels: standard configuration, conventional taildragger or tricycle to be determined
Floats: designed-in attachment points, float installation as an alternative configuration
The float attitude in the water is slightly less nose-up than the wheel ground attitude — managed by buoyancy geometry and float attachment point position, not by changing wing or stabilator incidence.
Structural Margins
Design gross weight: 2,000 lb
Target operating weight: 1,200–1,440 lb
Load factors: +3.8G / −1.5G limit, +5.7G / −2.25G ultimate (utility category)
The structural margin between operating weight and design weight provides room for growth without redesign. This is intentional.
BRS Parachute System
Under consideration. The operating weight class (~1,200–1,440 lb) falls within the BRS-1350 and BRS-2350 product range. The high-wing configuration deploys the chute upward with less risk of wing fouling than a low-wing design. Weight penalty approximately 25–30 lb installed. Minimum deployment altitude typically 300–400 ft AGL — adequate for open-water and cross-country use, less useful in a into-trees scenario at low altitude.
Attachment points to be designed into the fuselage primary structure: two forward at the firewall/instrument panel frame, two aft at the baggage bulkhead.
CHAPTER 11 — LANDING GEAR
Configuration
Conventional taildragger undercarriage with spring main gear legs and a steerable tailwheel. No retraction mechanism — the gear is fixed. This is the correct choice for a STOL bush aircraft: minimum weight, no actuators or hinges to fail, maximum ground clearance for the propeller on rough surfaces, and a straightforward float attachment geometry.
Main Gear — Grove 7075-T6 Spring Legs
Main gear legs are Grove Aircraft tapered spring legs, 7075-T6 aluminium. The tapered profile gives better energy absorption per unit weight than a straight-spring leg and is appropriate for the 1,200–1,440 lb operating weight range. Grove manufactures to order — leg length, axle position, toe-out angle, and gun-drill routing are all specified at time of order.
The 7075-T6 alloy is significantly stronger than the 6061 used in general structural applications and is the standard material for aircraft spring gear. It is not weldable in service — any damage to a spring leg means replacement, not repair. This is by design: a cracked or bent spring leg has unknown residual strength and must be treated as unairworthy.
Track Width
Target track width: 76 inches unloaded, approximately 82 inches at maximum gross weight (2,000 lb structural case). The spring legs splay outward under load as the spring deflects — the 6-inch spread across the weight range is a consequence of the leg geometry and is accounted for in the toe-out specification below.
For reference: Helio Courier track is approximately 84 inches, Cessna 185 approximately 88 inches. The Amihan's 76–82 inch range is slightly narrower but at a lower operating weight, giving a comparable rollover angle and ground stability margin.
Toe-Out
Slight toe-out is specified for ground dynamic stability. Toe-out gives each wheel a self-correcting rolling tendency when the aircraft yaws on the ground — each wheel's rolling resistance produces a restoring moment that resists the yaw rather than amplifying it.
Target: 1–2° toe-out measured at the unloaded axle position (76-inch track condition).
The critical stability case is minimum weight, not maximum gross weight. At minimum weight:
- The spring legs are least deflected — track is at its narrowest (76 inches)
- Moment of inertia about the vertical axis is lowest — the aircraft yaws more readily for a given side force
- The tailwheel carries less weight and has reduced steering authority
- Any crosswind or surface irregularity produces a larger yaw response relative to the available corrective moment
At maximum gross weight the legs are fully deflected, track is at its widest (82 inches), the aircraft is more resistant to yaw disturbance, and the tailwheel has greater authority. Ground stability is at its best when the aircraft is heavy — the wide track is doing the stability job, and a slight reduction in toe-out angle at that condition is acceptable.
Specify to Grove: 1–2° toe-out at the unloaded axle position. At max gross the toe-out will reduce to approximately 0.5–1° as the legs splay — this is the correct outcome. Do not specify toe-out at the loaded condition, as this would result in excessive toe-out at the minimum-weight case where it is most critical.
Gun-Drilled Hydraulic Lines
Grove gun-drills the hydraulic brake line through the interior of the spring leg from the fitting at the top of the leg to the caliper at the axle. No external hose runs on the exterior of the leg. This is the correct solution for the saltwater, gravel, and brush environment the Amihan operates in — external hoses on spring gear legs are vulnerable to abrasion from gravel throw, snagging on brush and rocks, and corrosion at the fittings. The internal line is fully protected by the leg itself and requires no additional chafe protection or routing hardware.
Wheels and Brakes
Grove supplies matched wheel, brake caliper, and rotor assemblies sized to the gear legs. The caliper mounts at the axle end of the gun-drilled line — no external hose at the wheel end.
Wheel and tyre size: to be confirmed. For gravel, beach, and rough-strip operation the target is a tyre in the 6.00×6 to 8.50×6 range. Larger tyres absorb more surface roughness, reduce the risk of a rock deflecting a wheel hard enough to upset the aircraft, and give more flotation on soft surfaces. The tyre selection should be confirmed against the ground clearance available under the fuselage at maximum spring deflection.
Leg Fairings and Wheel Pants
Leg fairings are two-piece clamshell fibreglass or carbon shells fitting around the spring leg from the fuselage attach point to the axle. At 150 knots cruise an unfaired spring leg produces significant profile drag — the fairings are worth the weight and complexity for this performance target.
Wheel pants are fitted to the axle outboard of the brake caliper. In a serious bush or float operation wheel pants are sometimes removed — they collect mud, gravel, and debris — but should be treated as standard equipment for cross-country cruise use. Design the pant attachment so it can be removed in the field without tools if conditions require it.
Master Cylinders and Pedals
Independent toe brakes on both sets of rudder pedals — pilot and co-pilot sides. Dual brakes are specified from the outset even if only the pilot side is initially plumbed. The pedal and master cylinder hard points on the co-pilot side are built into the fuselage floor structure at the time of construction; adding the co-pilot master cylinders and connecting the lines later is then a minor task rather than a structural modification.
Master cylinders mount at the top of each rudder pedal in the conventional toe-brake position. Each master cylinder feeds its respective main gear caliper via the gun-drilled leg — left pedal to left caliper, right pedal to right caliper. Differential braking supplements rudder authority during the landing roll and is the primary means of directional control once the aircraft is too slow for aerodynamic rudder effectiveness.
Tailwheel
Steerable tailwheel, connected to the rudder pedals via springs or a direct linkage. A locking or full-swivel castering mode for tight ground manoeuvring is worth specifying. Tailwheel size and type to be confirmed — a larger tailwheel (8–10 inch diameter) handles rough surfaces better and is less likely to dig into soft ground.
Float Installation
Float attachment hard points are designed into the lower fuselage structure from the outset — four hard points, one per float strut, with load-spreading doublers built into the fuselage frames at the appropriate stations. The main gear legs are removed when floats are fitted. The gun-drilled hydraulic lines terminate at the top of each leg at a standard AN fitting — disconnecting the legs for float installation is a matter of removing the attach bolts and unscrewing the hydraulic fitting, with no cutting or splicing of lines.
Structural Attachment
Spring gear legs attach to the fuselage at a single hard point per leg — typically a machined aluminium or steel socket or saddle welded or bolted to a primary fuselage frame. The attach fitting must be built into the fuselage primary structure, not added to the skin. Load path: spring leg bending and axial loads transfer through the attach fitting into the fuselage frame, which distributes them into the fuselage skin and longerons.
The attach fitting geometry is to be confirmed against Grove's standard leg interface dimensions once leg length and profile are specified. Grove provides dimensional drawings for all standard leg configurations — obtain these before finalising the fuselage frame layout at the gear station.